
Views: 236 Author: Dongguan PRES Publish Time: 2026-08-20 Origin: Site


Content Menu
● Why PEEK Is Machinable—but Demanding
● Why Sharp Tooling Matters in PEEK Machining
>> What Happens When Tools Become Dull
>> Recommended Tool Features for PEEK
● Why High Cutting Speeds Are Critical
>> The Correct Principle: Fast, Sharp, and Controlled
>> Starting Parameters for PEEK CNC Machining
● How to Machine PEEK Successfully
>> Start With Stable PEEK Stock
>> Use Rigid, Low-Stress Workholding
● Grade-Specific PEEK Machining Strategy
● Common PEEK Machining Problems and Fixes
>> Problem: Melted Surface or Glossy Smear
>> Problem: Burrs Around Holes and Milled Edges
>> Problem: Warpage After Machining
>> Problem: Rapid Tool Wear in Filled PEEK
● Expert Workflow for High-Precision PEEK Parts
● Partner With PRES for Machinable PEEK Materials
>> Why does PEEK need sharp cutting tools?
>> What cutting speed should be used for PEEK?
>> Does carbon-fiber PEEK require special tooling?
>> Should PEEK be annealed before machining?
>> Can PRES provide PEEK materials for OEM projects?
At Dongguan PRES Group Co., Ltd., we supply high-performance plastic materials for global brands, wholesalers, and manufacturers—including PEEK granules, sheets, rods, tubes, powders, and high-performance 3D-printing filaments. As a China-based OEM partner, we know that successful PEEK machining begins long before the CNC cycle: it starts with selecting stable, properly prepared material and applying the right tooling, cutting strategy, and heat-control discipline.
This PEEK machinability guide explains why sharp tooling and high cutting speeds are critical to producing accurate, clean, reliable PEEK components. Whether you machine natural PEEK, glass-filled PEEK, or carbon-fiber-reinforced PEEK, the objective is the same: create a clean chip, move heat away from the workpiece, and avoid stress, melting, burrs, dimensional drift, and surface damage.
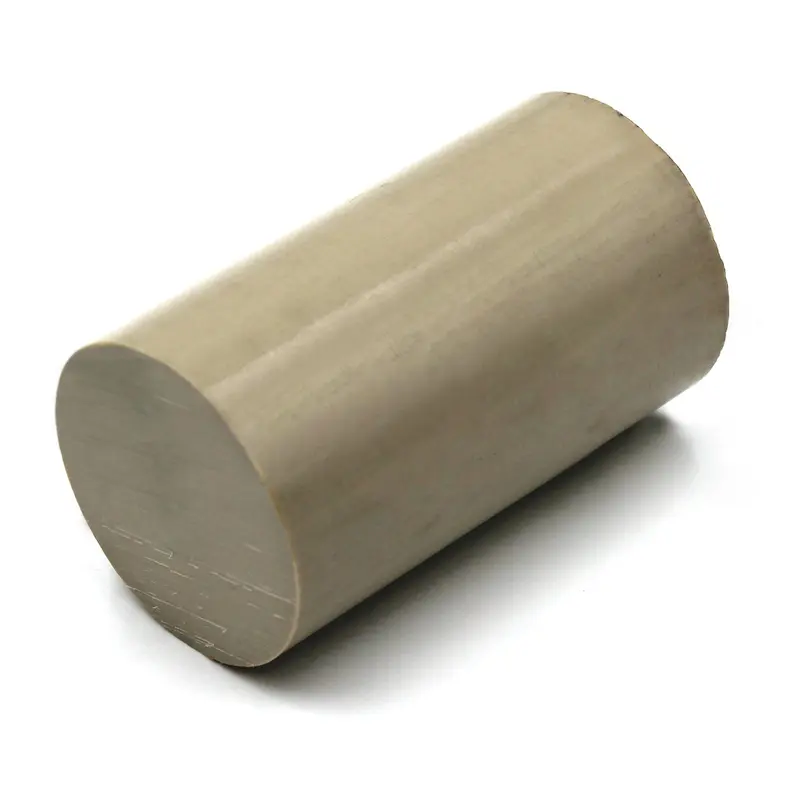
PEEK, short for polyether ether ketone, is a semi-crystalline high-performance thermoplastic. It is widely specified for applications that require heat resistance, chemical resistance, wear performance, electrical insulation, low weight, and long-term mechanical reliability.
Compared with metals, PEEK is easier to cut in some respects because it is lighter and creates lower cutting forces. However, it demands a different machining mindset. Metals can transfer heat relatively efficiently through the workpiece. PEEK has lower thermal conductivity, so frictional heat can concentrate quickly around the cutting edge and inside the part.
When heat is not controlled, the consequences can include:
- Smearing instead of clean material removal.
- Melted or re-solidified edges around holes, grooves, and pockets.
- Burr formation at exits and sharp transitions.
- Residual stress release, causing warpage after machining.
- Poor surface finish and inconsistent dimensions.
- Tool loading, where softened polymer adheres to the cutting edge.
- Cracking risk in stressed or heavily machined parts.
For this reason, PEEK machining is not simply "metal machining with plastic settings." It is a controlled process where material condition, tool sharpness, chip evacuation, workholding, speed, feed, depth of cut, and annealing all interact.
At PRES, we help OEM customers select PEEK material forms and grades that match their fabrication route—from prototype machining and high-volume CNC production to extrusion, injection molding, and additive manufacturing.
Sharp tooling is the first requirement for PEEK machinability. A sharp cutting edge shears PEEK cleanly. A dull edge rubs, compresses, and heats the polymer before it cuts.
This difference is fundamental. Cutting creates chips; rubbing creates heat.
A correctly sharpened tool reduces friction, improves chip formation, lowers machining forces, and protects surface integrity. Industry guidance for machining engineering plastics consistently emphasizes sharp, plastic-specific tool geometry and efficient heat dissipation through the chips.
A dull tool does not always produce an obvious failure immediately. In many PEEK projects, it first appears as a gradual quality decline:
- The surface becomes glossy, smeared, or streaked.
- Fine burrs increase around milled edges and drilled holes.
- The spindle load rises.
- Chips become powdery, melted, or inconsistent.
- Dimensional variation increases as the workpiece warms.
- Tight-tolerance components distort after unclamping.
This is especially critical when machining thin PEEK walls, asymmetrical components, deep pockets, medical parts, sealing elements, precision electrical insulators, and bearing components.
For natural or unfilled PEEK, sharp carbide tools are often an effective starting point. For reinforced grades, especially carbon-fiber-filled PEEK, more wear-resistant tooling such as diamond or PCD may be justified because the reinforcement accelerates edge wear.
A practical PEEK tooling strategy should include:
- Sharp cutting edges with no built-up material.
- Positive rake angles to support clean shearing.
- Polished flutes to reduce chip adhesion.
- Low-friction geometry designed for plastics rather than generic metal cutting.
- Adequate chip space, especially for slotting and deep milling.
- Limited flute count where chip evacuation is a priority.
- Frequent inspection of edge condition, not only catastrophic tool failure.
For reinforced PEEK, use tooling that matches the filler. Carbon fiber and glass fiber improve stiffness and dimensional stability in many applications, but they also make the machining environment more abrasive. A tool that performs well in natural PEEK may wear rapidly in a filled grade.
The phrase "high speed" can be misunderstood. In PEEK machining, it does not mean running every operation at the machine's maximum RPM. It means using a cutting speed high enough to create a clean, controlled shearing action while pairing it with suitable feed, chip load, chip evacuation, and cooling.
When the cutting speed is too low, the tool can rub instead of cut. That rubbing increases friction and deposits heat into the PEEK part. When a sharp tool runs at an appropriate speed, more heat can leave with the chip rather than remaining in the component.
Ensinger notes that because plastics have poor thermal conductivity, effective heat dissipation is essential, with chip removal being a primary route for carrying heat away from the cutting zone.
A successful PEEK machining process usually follows this hierarchy:
1. Use a sharp tool with the right geometry
2. Set cutting speed for clean shearing
3. Maintain a meaningful chip load
4. Remove chips immediately
5. Use compressed air or appropriate cooling when needed
6. Monitor heat, not only spindle speed
High speed without a sharp tool is not a solution. High speed with excessive feed can overload the edge. High speed with poor chip evacuation can melt chips into the cut. The goal is a stable process, not an aggressive number.
The following values are starting ranges, not universal production settings. Actual parameters must be validated according to PEEK grade, tool diameter, spindle capability, part geometry, workholding rigidity, tolerance requirement, and machine condition.
| Operation | Natural PEEK starting guidance | Carbon-fiber-reinforced PEEK starting guidance | Key process priority |
|---|---|---|---|
| Turning speed | 250–500 m/min | 150–200 m/min | Sharp insert and stable support |
| Turning feed | 0.1–0.5 mm/rev | 0.1–0.5 mm/rev | Avoid rubbing and heat buildup |
| Milling speed | 50–200 m/min | 200–300 m/min | Chip evacuation and clean edges |
| Drilling speed | 50–200 m/min | 80–100 m/min | Pecking and chip removal |
| Drilling feed | 0.1–0.3 mm/rev | 0.1–0.3 mm/rev | Prevent hole-wall smearing |
| Sawing speed | 500–800 m/min | 200–300 m/min | Sharp teeth and adequate feed |
These ranges are adapted from published PEEK machining guidance and should be treated as a process-development baseline rather than a substitute for validation trials.
Machining performance is strongly affected by the condition of the starting stock. A PEEK rod, sheet, tube, or plate can contain residual stresses from its manufacturing history. When heavy machining removes material asymmetrically, internal stresses may release and cause movement or warpage.
For precision components, start with well-conditioned, quality-controlled stock shapes. At PRES, we support customers with OEM supply of PEEK stock forms, helping align the material format with the part geometry and production method.
For high-precision parts, consider:
- Annealed PEEK stock for improved dimensional stability.
- Appropriate machining allowance before final finishing.
- Balanced material removal from opposing sides.
- Intermediate stress relief for deep pockets, thin walls, or highly asymmetric parts.
- Grade selection based on use conditions, not price alone.
Annealing can reduce residual stress, increase crystallinity, and improve dimensional stability. It becomes particularly valuable when a component has demanding flatness, roundness, concentricity, or tight-tolerance requirements.
PEEK is lighter and less rigid than metal. Excessive clamping force can deform the part during machining, then allow it to spring back after release. This can produce components that measure correctly in the fixture but fall out of tolerance afterward.
Use workholding that supports the component without crushing it.
- Support long rods during turning.
- Use soft jaws for delicate profiles.
- Avoid excessive chuck pressure.
- Machine thin walls progressively.
- Leave finishing allowance for the final pass.
- Recheck critical dimensions after unclamping and cooling.
For tubular PEEK parts, internal support may be necessary to prevent ovality. For plates, vacuum fixtures or broad support surfaces may be more effective than concentrated clamps.
A clean chip is one of the best indicators of a stable PEEK process. Chips should move away from the cutting zone quickly. If they pack into a drill hole, wrap around a tool, or melt into a slot, heat rises and quality falls.
Compressed air is often highly useful because it cools the cutting zone and clears chips simultaneously. For deep-hole drilling, thread cutting, and certain reinforced materials, additional cooling may be needed. Engineering-plastic guidance identifies deep drilling, threading, and sawing reinforced plastics as cases where cooling becomes especially important.
Use these practices:
- Direct compressed air at the cutting zone.
- Apply peck drilling for deep holes.
- Retract frequently to clear chips.
- Avoid dwelling at the bottom of a hole.
- Keep flutes free from packed material.
- Use coolant only after confirming material, cleanliness, and end-use requirements.
For medical, food-contact, or contamination-sensitive parts, dry machining with clean filtered air may be preferable. The machining environment, cleaning procedure, and traceability plan must be evaluated as part of the complete manufacturing process—not after the part is finished.
Not all PEEK grades respond the same way. A reliable machining plan begins by identifying whether the material is natural, glass-filled, carbon-filled, bearing-grade, conductive, medical-grade, or recycled-content modified.
| PEEK material type | Machining behavior | Best practice |
|---|---|---|
| Natural PEEK | Clean machining potential but sensitive to heat and stress | Use sharp carbide tools, clean chip evacuation, controlled speed |
| Glass-filled PEEK | More abrasive and potentially more brittle at edges | Use wear-resistant tooling and reduce edge chipping risk |
| Carbon-fiber PEEK | Abrasive, stiff, and often more dimensionally stable | Consider PCD or diamond tooling and control fiber-related surface effects |
| Medical-grade PEEK | Requires strict contamination control | Use validated clean machining methods and appropriate handling |
| Thin-wall PEEK | Prone to deflection and post-machining movement | Use low-stress fixturing, staged cuts, and final finishing passes |
An expert machining plan also considers fiber orientation. In reinforced extruded stock, fiber direction may influence cutting behavior, surface appearance, and the tendency for the part to move after material removal.
Likely causes include a dull tool, insufficient chip load, rubbing, poor chip evacuation, or excessive localized heat.
Corrective actions:
- Replace or regrind the cutting tool.
- Increase cutting efficiency rather than simply slowing the spindle.
- Confirm the tool is producing chips instead of dust.
- Improve air blast and chip removal.
- Reduce dwell time and repeated finishing passes.
Burrs usually indicate poor cutting action, unsupported material, worn edges, or an unsuitable exit strategy.
Corrective actions:
- Use a sharp drill or end mill.
- Add a backing plate for drilled exits.
- Reduce breakthrough aggression.
- Use controlled chamfering or deburring passes.
- Check workholding for vibration.
Warpage often results from residual stress release, uneven stock removal, excess machining heat, or inadequate support.
Corrective actions:
- Begin with annealed stock.
- Rough machine, stress-relieve if necessary, then finish machine.
- Remove material symmetrically.
- Reduce clamping stress.
- Let parts cool before final measurement.
This is common in glass-filled and carbon-fiber-filled PEEK because fillers are abrasive.
Corrective actions:
- Upgrade from standard carbide to coated carbide, diamond, or PCD where justified.
- Establish a tool-life limit before finish quality declines.
- Inspect cutting edges frequently.
- Separate parameters for natural and reinforced grades.
For customers developing demanding PEEK components, we recommend the following production workflow:
1. Confirm the application requirements
Define temperature, chemical exposure, mechanical load, electrical needs, cleanliness standards, and tolerances before selecting the grade.
2. Select the right PRES PEEK material form
Choose granules for molding, sheets for flat parts, rods for turned components, tubes for fluid or structural parts, powders for specialized processing, or filament for high-performance 3D printing.
3. Validate material condition
Review dimensions, batch consistency, internal stress condition, and any required documentation before machining.
4. Choose tooling by PEEK grade
Use sharp plastic-cutting geometry for natural PEEK and higher-wear-resistance tools for fiber-reinforced grades.
5. Run a controlled machining trial
Start with proven parameter ranges, then monitor chips, surface finish, part temperature, spindle load, burrs, and post-machining dimensions.
6. Use staged machining for complex parts
Rough machine first, allow stress to relax or perform intermediate annealing where appropriate, then finish machine.
7. Inspect after unclamping
Measure critical features after the part has cooled and been released from the fixture.
This workflow prevents the common mistake of optimizing cycle time before stabilizing part quality. In PEEK machining, a slightly slower but repeatable process is usually more profitable than fast production followed by scrap, rework, or inspection failures.
PEEK machinability depends on far more than CNC programming. Sharp tooling and high cutting speeds are critical because they promote clean shearing, efficient chip formation, and lower heat concentration in the part. But the strongest results come from combining this approach with stable PEEK stock, appropriate grade selection, controlled fixturing, proper annealing, and disciplined quality control.
Dongguan PRES Group Co., Ltd. supplies a broad range of high-performance plastic products for OEM projects worldwide. Whether you need PEEK granules, sheets, rods, tubes, powders, or advanced 3D-printing filaments, our team can help you evaluate the right material route for your product and manufacturing process.
Contact PRES today to discuss your PEEK material specification, OEM requirements, machining application, and custom product needs.
PEEK is machinable, but it requires more heat control and sharper tooling than many common plastics. Its low thermal conductivity means heat can accumulate near the cutting zone, causing smearing, burrs, stress, and dimensional changes if the process is not properly controlled.
Sharp tools shear PEEK cleanly and reduce friction. Dull tools rub against the material, generate excess heat, create poor chips, and increase the risk of melting, burr formation, and surface damage.
The right speed depends on the operation, tool diameter, PEEK grade, machine rigidity, cooling method, and required finish. Published guidance includes turning ranges of 250–500 m/min for natural PEEK and 150–200 m/min for carbon-fiber-reinforced PEEK, but production settings should always be validated through machining trials.
Yes. Dry machining is often possible when chip removal and air cooling are effective. However, deep drilling, thread cutting, and reinforced-material sawing may require additional cooling or lubrication strategies.
Usually, yes. Carbon fiber is abrasive and can wear standard cutting edges quickly. Diamond, PCD, or other wear-resistant tools can improve tool life and maintain surface quality, particularly in repeated production runs.
Annealing is strongly recommended for precision PEEK components, heavily machined parts, thin-wall parts, or applications with tight tolerances. It reduces residual stress and can improve dimensional stability after machining.
Yes. Dongguan PRES Group Co., Ltd. provides OEM-oriented high-performance plastic products, including PEEK pellets, sheets, rods, tubes, powders, and 3D-printing filaments for international brands, wholesalers, and manufacturers.
1. [Victrex PEEK Finishing Operations Guide] — Manufacturer resource on finishing and machining operations for PEEK-based materials. [victrex]
2. [Ensinger: Frequently Asked Questions for Machinable Plastics] — Guidance on sharp tools, plastic-specific geometry, chip-based heat dissipation, cooling, annealing, drilling, turning, and dimensional stability. [ensingerplastics]
3. [AIP Precision Machining: Machining PEEK—A Plastics Guide] — Overview of PEEK machining, annealing, tooling choices, cooling practices, and starting ranges for sawing, drilling, milling, and turning. [aipprecision]
Hot Tags: China, Global, OEM, private label, manufacturers, factory, suppliers, manufacturing company


