
Views: 231 Author: Dongguan PRES Publish Time: 2026-08-26 Origin: Site


Content Menu
● Why PEEK Valve Plates Matter in Oxygen Systems
● PEEK Advantages for Precision Valve Plates
>> Key performance benefits of PEEK valve plates
● The Main Ignition Risks in Oxygen Valve Assemblies
>> Adiabatic compression during rapid pressurization
>> Particle impact and flow impingement
>> Mechanical friction, rubbing, and compression
>> Contamination from oil, grease, fibers, and particles
● Why "PEEK Grade" Is Not Enough
● A Practical Engineering Workflow for PEEK Valve Plates
>> 1. Start with the valve risk map
>> 2. Specify the correct PEEK material form
>> 3. Engineer geometry for lower ignition exposure
>> 4. Validate the complete assembly
● Clean Manufacturing Is a Safety Requirement
>> Oxygen-clean manufacturing controls to request
>> Customer feedback themes we hear from OEM buyers
● PEEK Valve Plate Design Checklist
● Partner With PRES for Custom PEEK Valve Plates
● FAQ
>> Is PEEK safe for oxygen systems?
>> Can PEEK valve plates be used in high-pressure oxygen valves?
>> What is the greatest ignition risk for a PEEK valve plate?
>> Should a PEEK valve plate be directly exposed to oxygen flow?
>> What documentation should I request from a PEEK valve plate supplier?
>> Does CNC machining affect PEEK valve plate quality?
At Dongguan PRES Group Co., Ltd., we manufacture high-performance PEEK materials and precision plastic components for international brands, wholesalers, and manufacturers. For engineers specifying PEEK valve plates in oxygen systems, the central question is not simply whether PEEK is heat-resistant or mechanically strong—it is whether the complete valve design, material grade, cleanliness standard, operating pressure, and possible ignition sources have been evaluated together.
PEEK can be an excellent engineering polymer for demanding valve applications because it combines high strength, thermal stability, chemical resistance, and dimensional control. However, PEEK is not automatically "oxygen-safe" in every application. In oxygen-enriched or high-pressure oxygen systems, every nonmetallic part must be assessed for its real service environment, including rapid pressurization, particle impact, adiabatic-compression heating, contamination, friction, and failure consequences. NASA research has specifically evaluated PEEK among polymers for particle-impact ignition behavior in oxygen environments, underscoring that polymer selection must be evidence-based rather than assumed.
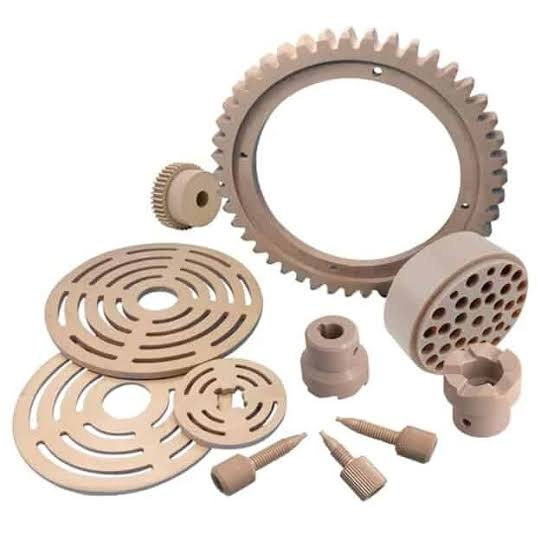
A valve plate controls, directs, separates, or seals gas flow within a valve assembly. Depending on the valve design, it may act as a sealing interface, guide plate, flow-control element, insulating component, or structural element supporting other moving parts.
In oxygen service, a valve plate may be exposed to conditions far more severe than ordinary industrial gas handling:
- High oxygen concentration
- High operating pressure
- Rapid valve opening or pressurization
- High-velocity gas flow
- Particles or metallic debris
- Repeated mechanical cycling
- Temperature variation
- Cleaning and handling risks
Oxygen itself is not a fuel. The danger is that oxygen strongly accelerates combustion when a heat source and fuel are present. A polymer valve plate can become part of the fuel load if it is exposed to an ignition event. Therefore, an oxygen-compatible valve is not created by selecting one "good" plastic. It is created by controlling the entire system: materials, geometry, flow path, assembly, cleanliness, validation, and operating limits.
For OEM buyers, this distinction is essential. A PEEK valve plate that performs well in compressed air, nitrogen, water, or chemical processing cannot automatically be transferred to gaseous oxygen, liquid oxygen, medical oxygen, aerospace oxygen, or high-pressure industrial oxygen service.
PEEK, or polyether ether ketone, is a high-performance thermoplastic widely chosen for severe mechanical, thermal, and chemical environments. For valve plates, its practical value is often found in the balance between rigidity, machinability, low moisture absorption, and long-term dimensional stability.
At PRES, our approach starts with the intended function of the part—not only the resin name. We support PEEK raw material, PEEK sheets, rods, tubes, powders, and customized machined or molded components for OEM applications. This gives product-development teams flexibility to select the right format for prototyping, validation, low-volume production, and scaled manufacturing.
| Requirement | Why it matters in a valve plate | Potential PEEK benefit |
|---|---|---|
| Dimensional stability | Valve plates often require controlled flatness and fit | Helps maintain geometry in demanding thermal and mechanical conditions |
| Mechanical strength | The plate may face compression, cycling, and differential pressure | Offers strong load-bearing performance compared with many commodity plastics |
| Thermal resistance | Valve components can encounter heat from friction, compression, or nearby processes | Supports use in higher-temperature engineering environments |
| Chemical resistance | Cleaning agents, process media, or surrounding chemicals may be present | Resists many aggressive chemical environments |
| Low moisture absorption | Moisture-related dimensional changes can affect fit and sealing | Supports repeatable component dimensions |
| Precision machinability | Ports, grooves, channels, and sealing faces require accuracy | Can be CNC machined into complex valve plate geometry |
These properties make PEEK a strong candidate when the design requires more than basic plastic performance. Yet in oxygen service, mechanical capability does not replace oxygen-compatibility testing or system-level risk assessment.
The most reliable way to reduce risk is to understand how ignition can begin. In high-pressure oxygen systems, ignition is often caused by a combination of oxygen, heat generation, fuel, and a local event that concentrates energy.
When oxygen enters a closed or partially closed volume quickly, the gas temperature can rise sharply. This is commonly called adiabatic-compression heating. If the local temperature becomes high enough, a polymer, lubricant, contaminant, or other combustible material can ignite.
Research on pneumatic-impact ignition identifies adiabatic-compression heating as a likely cause of polymer ignition in high-pressure oxygen systems. PEEK has been included among the polymers tested under these conditions, reinforcing the need to evaluate the actual pressure transient rather than only steady-state pressure.
Design response: Control opening speed, reduce sudden pressure differentials, avoid trapped volumes where practical, and review dead-end geometry.
A small particle carried by high-velocity oxygen can strike a surface and generate local heating. In some cases, this heat can ignite a nonmetallic component or contamination. NASA identifies particle-impact ignition as a primary cause of numerous oxygen-system fires and tested polymeric materials, including PEEK, for ignition resistance.
Design response: Minimize direct flow impingement on nonmetallic parts, control particle contamination, and use appropriate filters upstream.
Valve plates may contact mating parts repeatedly. Poor flatness, excessive preload, misalignment, rough surfaces, or incompatible lubricants can generate heat. Wear particles may also become a secondary hazard.
Design response: Define surface-finish requirements, control tolerances, validate cycling performance, and avoid unapproved lubricants or assembly compounds.
Contamination is among the most preventable oxygen-system hazards. Hydrocarbon residue, handling oil, packaging debris, machining coolant, lint, fingerprints, and loose particles can become fuels in an oxygen-rich environment.
Design response: Specify oxygen-clean manufacturing, dedicated cleaning procedures, controlled packaging, and traceable inspection before shipment.
A common sourcing error is to request "PEEK valve plates" without defining the operating conditions. This leaves too much uncertainty for a safety-critical oxygen application.
A responsible material-selection process should define:
1. Oxygen type: Gaseous oxygen, oxygen-enriched air, liquid oxygen, medical oxygen, or mixed gas.
2. Maximum operating pressure: Include normal operating pressure, proof pressure, surge pressure, and rapid-fill conditions.
3. Maximum and minimum temperature: Consider local hot spots and transient heating, not only room-temperature operation.
4. Valve geometry: Identify impingement zones, dead legs, narrow passages, seat interfaces, and trapped volumes.
5. Flow conditions: Define flow rate, opening speed, cycling frequency, and pressure-drop profile.
6. Contact materials: Review metals, seals, coatings, lubricants, adhesives, thread lockers, and filters.
7. Cleanliness requirement: Define the cleaning standard, inspection criteria, packaging method, and handling controls.
8. Required verification: Determine the relevant oxygen-compatibility tests and qualification documentation.
Guidance covering nonmetallic materials in oxygen systems emphasizes that selection should consider mechanical and chemical suitability, operating conditions, oxygen-compatibility data, auto-ignition behavior, and—as appropriate—gaseous-fluid-impact or mechanical-impact test results. It also calls for a meaningful temperature margin between operating conditions and a material's measured ignition threshold.
At PRES, we recommend treating oxygen valve plate development as a controlled engineering project rather than a standard plastic-part purchase.
Before selecting a PEEK grade or drawing the final geometry, identify where energy can be released:
- Rapid inlet pressurization
- High-velocity gas impingement
- Metal-to-metal impact
- Sliding or rubbing interfaces
- Particle accumulation areas
- Sharp internal corners
- Polymer exposure in the primary flow stream
- Interfaces containing lubricants, seals, or adhesives
The objective is to prevent the PEEK valve plate from being placed in the highest-risk location when a metal alternative, shield, geometry change, or flow-control feature is feasible.
PRES can supply PEEK in multiple product forms, including pellets, sheet, rod, tube, powder, and 3D-printing filament. For oxygen valve plates, the chosen form should match the manufacturing process and performance requirement.
| Manufacturing path | Best use case | Engineering consideration |
|---|---|---|
| CNC-machined PEEK sheet | Prototypes, precision low-to-medium volumes, complex features | Allows close control of geometry and finishing |
| Injection-molded PEEK | Higher-volume repeatable parts | Requires tooling optimization and qualified processing parameters |
| Compression-molded or formed PEEK | Specific plate geometries and production needs | Requires uniform processing and quality control |
| PEEK powder | Specialized forming or compounding workflows | Must be controlled for purity and process consistency |
| PEEK filament | Functional prototypes and fixture development | Not a substitute for validated final oxygen-service components without qualification |
For oxygen applications, avoid assuming that a prototype made by one process has the same surface condition, density, defect profile, or performance as a production part made by another process.
The valve plate should support safe flow behavior, not create new hazards. Where the system design permits, consider:
- Reducing direct oxygen impingement on the polymer surface
- Avoiding sharp transitions that increase turbulence
- Limiting thin sections near high-energy flow paths
- Controlling concentricity and flatness at sealing interfaces
- Designing ports with smooth, repeatable edges
- Preventing loose debris generation through robust edge finishing
- Using metallic barriers or seats in the most severe impingement areas
A polymer can perform acceptably as a test coupon and still fail in a real valve because the assembly introduces friction, pressure transients, contamination, or metal ignition mechanisms.
NASA guidance warns against qualifying oxygen-service materials solely through one test method. It recommends a system hazards analysis that considers ignition sources, likelihood, severity, appropriate test methods, and safety margin.
For critical applications, validate the final configuration—including the valve body, PEEK plate, seals, fasteners, surface treatment, cleanliness process, and intended operating cycle.
In our experience serving overseas OEM customers, quality is not complete when a PEEK valve plate meets its drawing dimensions. For oxygen-related use, cleanliness and packaging become part of the product specification.
- Controlled raw-material identification and batch traceability
- Machining processes that minimize contamination
- Appropriate coolant and cleaning-process management
- Deburring that prevents loose particles
- Inspection for visible residues, chips, fibers, and surface damage
- Defined washing, drying, and handling procedures
- Clean gloves and clean assembly practices
- Protective packaging that reduces recontamination during transport
- Lot labeling and inspection documentation
This is especially important because oxygen-system guidance identifies contaminants such as lubricant and organic materials as ignition concerns.
Across high-performance plastic sourcing projects, customers consistently value three outcomes:
- Stable dimensions: They need valve plates that fit consistently across production batches.
- Responsive engineering support: They need fast feedback when drawings, tolerances, or materials must be adjusted.
- Reliable export execution: They need consistent identification, protective packaging, and documentation for global supply chains.
These expectations shape our OEM service model at Dongguan PRES Group Co., Ltd. We work with customers on material form, machining feasibility, tolerance review, prototype development, batch consistency, and packaging requirements—rather than treating a high-performance component as a generic catalog item.
Before approving a PEEK valve plate for oxygen-system development, confirm the following:
- The maximum pressure and transient pressure conditions are documented.
- The oxygen concentration and temperature range are documented.
- The PEEK grade and manufacturing route are specified.
- The part's position in the gas-flow path is understood.
- Direct impingement and high-velocity particle paths are reviewed.
- All adjoining metals, seals, lubricants, adhesives, and coatings are identified.
- Cleaning and contamination-control requirements are written into the purchase specification.
- The component has required dimensional, surface-finish, and visual-inspection criteria.
- The full valve assembly has a documented oxygen fire-risk assessment.
- Required oxygen-compatibility testing is defined by the responsible engineering authority.
Dongguan PRES Group Co., Ltd. supplies high-performance PEEK materials and custom plastic solutions for global OEMs, brand owners, wholesalers, and manufacturers. Whether you need precision-machined PEEK valve plates, PEEK sheet for in-house machining, rods, tubes, pellets, powder, or high-performance 3D-printing filament, we can support your development and supply requirements.
For oxygen-system applications, send us your drawing and project conditions: material grade, dimensions, tolerances, annual quantity, working pressure, temperature range, cleanliness expectation, and application environment. Our team can help evaluate manufacturability and prepare a PEEK valve plate solution aligned with your production needs.
Contact PRES today to discuss your custom PEEK valve plate project and request a technical quotation.
PEEK may be suitable for certain oxygen-service applications, but it must not be considered universally safe without evaluating the specific pressure, temperature, flow, contamination level, geometry, ignition mechanisms, and required test evidence. Oxygen compatibility is determined at the system level, not by polymer name alone.
They can be considered, but high-pressure oxygen service requires a rigorous risk assessment. Rapid pressurization, particle impact, pneumatic impact, and local heating can create ignition hazards. The final design should be validated under relevant service conditions.
There is no single risk for every valve, but common hazards include adiabatic-compression heating, particle impact, high-velocity oxygen impingement, mechanical friction, and hydrocarbon contamination. The greatest risk depends on the valve's pressure-transient profile and geometry.
That decision should be based on an engineering risk assessment. Guidance generally advises minimizing nonmetallic materials directly in oxygen flow paths where feasible, particularly in high-energy or impingement locations.
Request material identification, batch traceability, dimensional-inspection records, surface-finish requirements, cleaning and packaging specifications, manufacturing-process details, and any agreed project-specific validation documentation. For critical oxygen service, your responsible engineering team should also define the required compatibility test evidence.
Yes. Machining parameters, tooling condition, coolant control, deburring, surface finishing, cleaning, and packaging can affect surface quality, particle generation, dimensional repeatability, and contamination risk. These factors should be controlled and documented for oxygen-related applications.

1. NASA Technical Reports Server, "[Ignition Resistance of Polymeric Materials to Particle Impact in High-Pressure Oxygen]."
2. Fire and Materials, "[Pneumatic Impact Ignition of Selected Polymers in High-Pressure Oxygen]."
3. NASA Technical Note, "[Some Issues Related to the Selection of Polymers for Aerospace Oxygen Systems]."
4. WHA International, "[Oxygen Compatibility and Safe-Use Criteria]."
5. WHA International, "[Nonmetals Oxygen Compatibility Requirements: Guide to CGA G-4.4, EIGA Doc 13 and CGA G-4.14/EIGA Doc 200]."
6. Swagelok, "[Materials for Industrial Oxygen Service: Ignition Mechanisms and Material Selection]."
7. Swagelok, "[Oxygen System Safety]."
8. Dive Gear Express, "[Material Guidelines for Gaseous Oxygen Service]."
Hot Tags: China, Global, OEM, private label, manufacturers, factory, suppliers, manufacturing company


