Views: 220 Author: plastic-material Publish Time: 2025-12-05 Origin: Site


Content Menu
● The Two Monomers: Hydroquinone and DFBP
● From Resin Powder to Pellets
● What Goes Into Modified PEEK Grades
● Properties That Come From This Chemistry
● From Pellets to Stock Shapes: How PRES Processes PEEK
>> Source PEEK Resin and Stock Shapes Factory-Direct
PEEK material is made of two aromatic monomers — hydroquinone and 4,4'-difluorobenzophenone (DFBP) — polymerized by nucleophilic aromatic substitution into polyetheretherketone, a semi-crystalline polymer of the PAEK family. No bisphenol A, no plasticizers: the finished polymer contains only carbon, hydrogen, and oxygen arranged in alternating ether and ketone links on benzene rings. Modified grades then add glass fiber, carbon fiber, or solid lubricants to the base resin. Here is exactly what goes into PEEK, step by step.
| Component | Chemical Role | What It Contributes to PEEK |
|---|---|---|
| Hydroquinone C6H4(OH)2 | Diphenol monomer — its two -OH groups are converted to phenoxide salts by the base, then attack the DFBP fluorine positions | The flexible ether linkages (C–O–C) — toughness, melt processability |
| 4,4'-Difluorobenzophenone (DFBP) C₁₃H₈F₂O | Activated difluoro monomer — the ketone group withdraws electrons, making the two C~F bonds easy to displace | The rigid ketone groups (C=O) on benzene rings — heat resistance, strength, crystallinity |
| Sodium carbonate (base) | Converts hydroquinone into reactive phenoxide and binds the displaced fluorine as NaF | Removed by washing after polymerization— not part of the final polymer |
| Diphenyl sulfone (solvent) | High-boiling solvent that keeps the reaction homogeneous at 300~320°C | Purged to trace levels — high-purity PEEK grades verify this in CoA |
PEEK is built by step-growth nucleophilic aromatic substitution (NAS). In simplified form:
n HO–C6H4–OH + n F–C6H4–CO–C6H4–F → [–O–C6H4–O–C6H4–CO–C6H4–]n+ 2n HF (captured as NaF)
Key conditions that decide final resin quality:
Strict 1:1 monomer ratio — step-growth chemistry only reaches high molecular weight when the two monomers are balanced to within fractions of a percent.
Temperature 300~320°C in diphenyl sulfone — hot enough for substitution, below PEEK's melting point of 343°C so the growing chains stay processable.
Anhydrous conditions — water would cap growing chain ends and limit molecular weight.
Precise end-group control — resin for extrusion (high viscosity) and injection molding (standard flow) is tuned by molecular weight and end-capping.
The reactor discharge is raw PEEK powder carrying salts and solvent residue. Before it becomes usable material it goes through:
Crushing & multi-stage washing — removes NaF, sodium salts, and residual diphenyl sulfone;
Drying & sieving — moisture control to ppm level prevents hydrolytic molecular-weight loss during melt processing;
Melt extrusion & pelletizing — the powder is melted and cut into the standard pellets used for molding and extrusion, or compounded with fillers to make modified grades;
Quality control — melt flow index, molecular weight, purity (ash, volatile content), and for medical/semiconductor grades, full impurity profiling. Our PEEK pellets >> page covers the resin grades we stock.
"PEEK" on a datasheet is rarely 100% neat resin. The five grades we produce differ only in what is compounded into the same base polymer:
| Grade | What Is Added | What It Changes |
|---|---|---|
| Unfilled (virgin) | Nothing — 100% PEEK resin | Highest toughness (45% elongation) and purity; tensile strength 100 MPa |
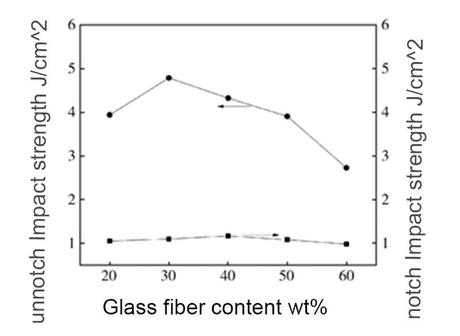
| GF30 | 30% short glass fiber | Stiffness ×3 (flexural modulus 11 GPa), HDT up to 315°C, lower cost per stiffness |
| CF30 | 30% carbon fiber | Tensile 250 MPa, modulus 23 GPa, thermal conductivity 0.95 W/(m·K), CLTE down to 15 ppm/K — but electrically conductive |
| Bearing grade | Carbon fiber + graphite + PTFE solid lubricants | Low friction and wear for dry-running bushings and seals; HDT 293°C |
| ESD / anti-static | Conductive carbon-based filler, dosage-controlled | Volume resistivity tuned to 106~109 Ω·cm for electronics handling |
The alternating ether–ketone backbone is directly responsible for the numbers that make PEEK famous (values: unfilled grade, ISO standards):
Melting point 343°C / Tg 143°C — from the rigid ketone-linked aromatic rings (ISO 11357);
Continuous service temperature 260°C, short-term peaks to 300°C — semi-crystalline stability with no additives;
Tensile strength 100 MPa, elongation 45% — the ether links keep it tough, not brittle (ISO 527);
Density 1.30 g/cm3, water absorption 0.07% in 24h — a tight, hydrophobic aromatic backbone (ISO 1183 / ISO 62-1);
Chemical resistance — the C~F-derived ether bonds are stable against nearly all solvents, oils, and fuels.
Full grade-by-grade data: PEEK material selection guide >> | Broader overview: What is PEEK material? >>
Because PEEK is a thermoplastic, the same resin can be re-melted and formed repeatedly — which is how one material serves three very different production routes:
Extrusion into sheet, rod, tube, and film — followed by in-house stress-relief annealing, so machined parts stay flat and dimensionally stable;
Injection molding at 360~400°C for high-volume parts — mold temperature above Tg (143°C) is critical to build crystallinity;
CNC machining from annealed stock shapes for prototypes and low-volume precision parts — chips are reground and reused where purity allows.