Views: 220 Author: plastic-material Publish Time: 2025-12-23 Origin: Site


Inherent flame resistance (LOI 44–47%, V-0 at 0.4 mm unmodified)
Inherent chemical inertness to fuels, oils, acids, and bases
Fast crystallization → low mold shrinkage, short cycle times, excellent dimensional stability
| Property | Unfilled PPS | 40% GF PPS | Test Standard |
|---|---|---|---|
| Density | 1.34 g/cm³ | 1.67 g/cm³ | ISO 1183 |
| Melting Point (Tm) | 278–285°C | 278–285°C | DSC |
| Glass Transition (Tg) | 85–90°C | 85–90°C | DSC |
| Continuous Service Temp | 200–220°C | 200–220°C | UL 746B |
| Tensile Strength | 65–80 MPa | 160–190 MPa | ISO 527 |
| Flexural Modulus | 3,500–4,000 MPa | 12,000–15,000 MPa | ISO 178 |
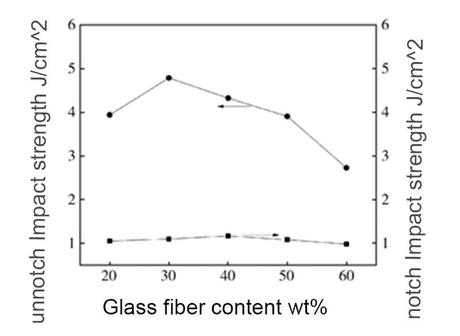
| Notched Izod Impact | 25–50 J/m | 50–80 J/m | ISO 180 |
| Elongation at Break | 2–5% | 1–2% | ISO 527 |
| HDT (1.8 MPa) | 115–135°C | 255–270°C | ISO 75 |
| Mold Shrinkage (flow) | 0.5–1.0% | 0.1–0.3% | ISO 294 |
| Water Absorption (24h) | 0.02–0.05% | 0.02–0.05% | ISO 62 |
| Flammability | UL 94 V-0 | UL 94 V-0 | UL 94 |
| Volume Resistivity | 10 16 Ω·cm | 10 16 Ω·cm | IEC 60093 |
The single number engineers misuse most: HDT of unfilled PPS is only ~115°C because Tg is 85–90°C. Reinforcement (GF/mineral) is what pushes HDT past 250°C—never specify "PPS" for a 200°C-load part without stating the reinforced grade.
Dry resin first: 150°C for 3–4 h (even though absorption is low, surface moisture causes silver streaks and hydrolytic chain scission at 300°C+)
Melt temperature: 300–340°C (typical 315–325°C for GF grades)
Mold temperature: 120–150°C (higher mold temp = higher crystallinity = better HDT and less post-mold warpage)
Cycle time: 20–40% shorter than PEEK; standard nitrided screw works, no 400°C barrel needed
Shrinkage & weld lines: flow-direction shrinkage 0.1–0.3% (GF40), but weld-line strength retention is only 50–70% of parent—gate placement matters in connector programs
Emissions: trace sulfur compounds off-gas at melt; vent the barrel zone, avoid breathing zone exposure
Automotive: EGR valves, thermostat housings, water-pump impellers, fuel-rail components, EV motor bobbins (≤180°C, coolant/oil contact, cost-critical)
Electronics: SMT connectors, relay bodies, coil formers, breaker arc-chambers (V-0 + low CLTE + survives lead-free reflow ~260°C peak)
Industrial: chemical pump housings, filter plates, valve liners, burner nozzles
Semi/Electrical: tray holders, test sockets—only when ion extractables and steam cycles allow; otherwise PEEK
Appliances: coffee-machine brew groups, oven fan housings
| Dimension | PPS | PEEK |
|---|---|---|
| Melting Point | 280°C | 343°C |
| Continuous Use | 200–220°C | 250–260°C |
| Tg | 85–90°C | 143°C |
| Tensile (neat) | 70 MPa | 95–110 MPa |
| Elongation (neat) | 2–5% | 40–45% |
| Melt Temp (process) | 300–340°C | 360–400°C |
| Izod Notched (GF30) | 50–80 J/m | ~90 J/m |
| Steam/AUTOCLAVE | Moderate (degrades faster) | Excellent (134°C ×3000+) |
| Cost (pellets) | $15–25/kg | $75–110/kg |
| Best fit | High-vol, ≤200°C, static, flame+chem | >220°C, impact/fatigue, medical/semi |